Qualify Real Candy Flow, Giveaway & Seal Integrity Before Shipment
Testing a candy weigher on dry plastic pellets hides sticky gummy hang-ups, sugar-dust seal leaks, and hard-candy chipping. Anchored in candy machine selection and sizing and candy weighing and dosing specs, ship 25–50 kg of real coated confectionery and two rolls of production film (or 300 premade pouches) for wet FAT qualification.
Record 100 consecutive production bags at target BPM to verify both mean overfill and zero-underweight compliance.
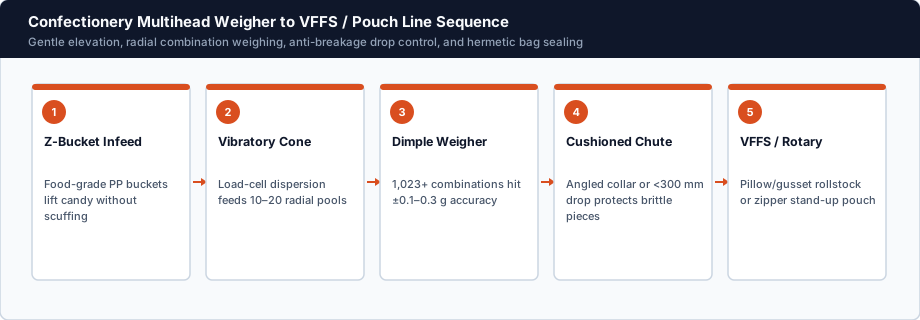
Confectionery FAT Qualification Checklist
Require pass sign-off across all five confectionery test criteria:
| FAT Criterion | Test Method | Confectionery Acceptance Target |
|---|---|---|
| 1. Continuous Sticky Flow | 30-min uninterrupted run on oiled/sugared candy | Zero radial cone bridging; tare drift <0.2 g between auto-zeros |
| 2. Weight / Count Accuracy | 100 consecutive bags weighed on calibrated scale | Zero underweight packs; mean giveaway within ±0.15–0.35 g |
| 3. Breakage & Stick Jam Audit | Open & inspect 50 finished hard-candy / lollipop bags | <0.1% chipped pieces; zero punctured film or stick jams |
| 4. Cross-Seal & Zipper Test | Vacuum tank (-0.06 MPa) + manual zipper re-close | Zero micro-leaks through sugar dust; 100% smooth zipper track |
| 5. Washdown Disassembly | Timed strip & re-hang of pans, chutes, and buckets | Tool-free strip completed in <15 minutes; auto-calibration clean |
Review turnkey integration deliverables on turnkey candy packaging lines.
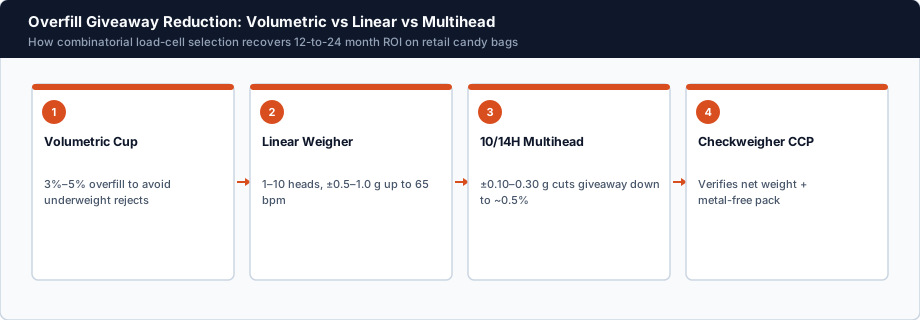
Confectionery Engineering Details
- Collect Forming Collar & Gripper Drawings: Archive exact dimensions of every forming tube and pouch gripper jaw for rapid future reorders.
- Verify HMI Recipe Presets: Pre-save vibration amplitudes, hopper dwell delays, and jaw temperatures for each SKU before crating.
- Inspect Spares Kit: Confirm spare PTFE tapes, cutter blades, silicone vacuum cups, timing belts, and heater cartridges are packed.
Start Your Confectionery RFQ
Attach this FAT checklist to your equipment inquiry so every vendor quotes to the same hygienic and accuracy standard.
Submit your candy line parameters via our Project Brief.
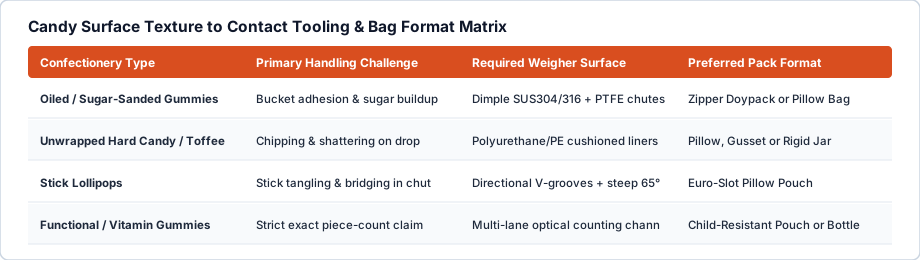
Compare related confectionery systems in Candy Packaging Machines, Weighing & Dosing Specs, or send your candy specs via Project Brief.