Product Physics Set Hopper Angles, Coatings & Drop Chutes
Treating oiled pectin gummies, brittle boiled hard drops, and stick lollipops as generic ‘granules’ causes bridged chutes, shattered candy shards in seals, and 40% OEE losses. Built under candy weighing and dosing specs, explore dedicated guides for hard candy and lollipop anti-breakage bagging and VFFS vs premade pouch candy comparisons.
Every confectionery family demands tailored contact metallurgy, chute inclination, and thermal ambiance.
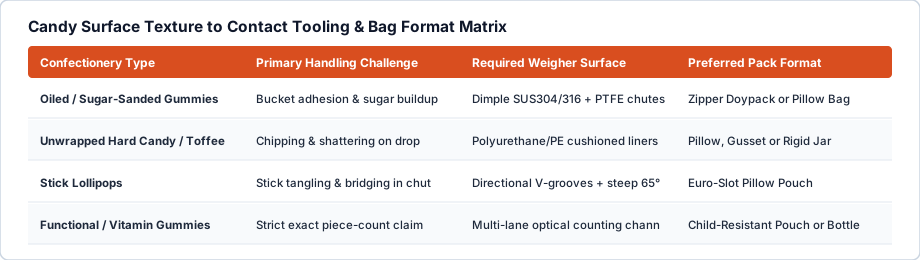
Product-Specific Tooling Configuration Table
Verify that all four mechanical adaptations are specified for your confectionery category:
| Confectionery Product | Contact Plate & Coating | Chute & Drop Design | Ambient / Gas Requirement |
|---|---|---|---|
| Pectin / Gelatin Gummies | Dimple SUS316 + PTFE coated funnel | Steep 60°–65° discharge + scraper gates | 45%–55% RH, 18–22 °C room air |
| Unwrapped Hard Boiled Candy | PU/PE cushioned bucket & collar liners | Low <300 mm drop or sloped spiral chute | Dry <45% RH air shroud to stop graining |
| Stick Lollipops | V-groove directional linear pans | Anti-tangle gate + stick alignment funnel | Reinforced puncture-resistant PE film |
| Chocolate Bites & Panning | Smooth cool SUS304 + gentle vibration | Soft-belt Z-elevator + chilled room (<20 °C) | Cold-jaw isolation + N2 gas flush |
Cross-reference speed and giveaway numbers in candy packaging machines.
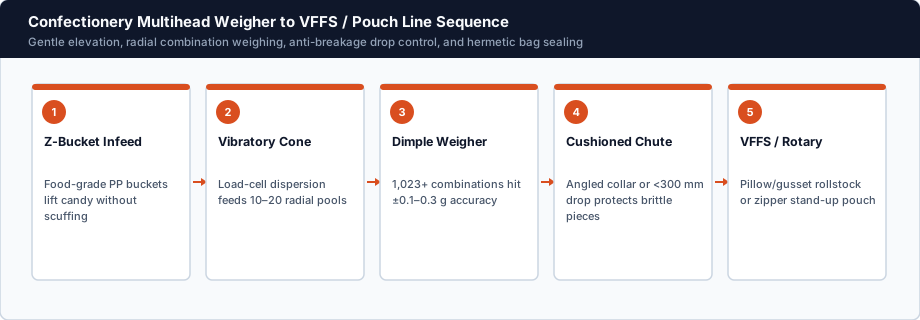
Confectionery Engineering Details
- Puncture-Resistant Film Selection: Lollipop sticks and sharp hard-candy edges require tougher 70–100 μm PET/LLDPE laminates rather than thin brittle BOPP.
- Scraped & Timed Timing Hoppers: Adding a bottom timing hopper right above the VFFS collar shortens free-fall distance and tightens high-speed jaw timing up to 120 BPM.
- Quick-Release Wet Sanitation: Gummy oil and citric dust build up over 1–2 shifts; tool-less bucket removal cuts wash-and-dry turnaround.
Send Real Production Candy for Live Drop & Flow Trials
Always test coated, cured candies at the exact temperature and oil/sugar finish they reach the packaging room.
Describe your candy formulation on our Project Brief.
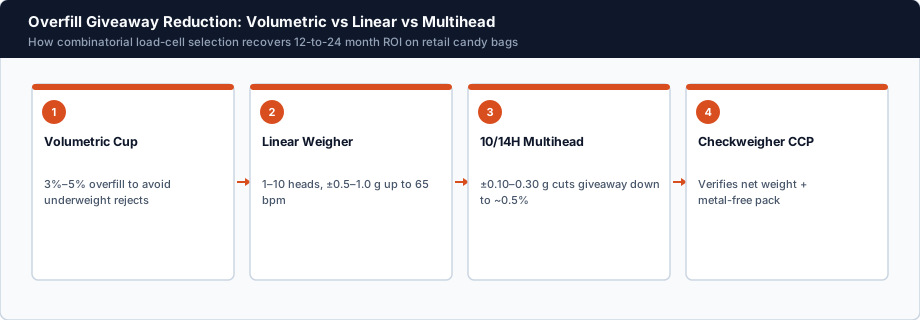
Compare related confectionery systems in Candy Packaging Machines, Weighing & Dosing Specs, or send your candy specs via Project Brief.
In This Section
Related Specifications
Further Reference
- Candy Packaging Machines: How to Specify by Confectionery Type, Bag Format & Speed
- Confectionery Weighing & Dosing Specifications: Multihead vs Linear vs Counting
- Hard Candy, Toffee & Lollipop Bagging: Anti-Breakage & Stick Alignment
- VFFS Rollstock vs Rotary Premade Pouch: Confectionery Speed, Cost & Shelf Appeal